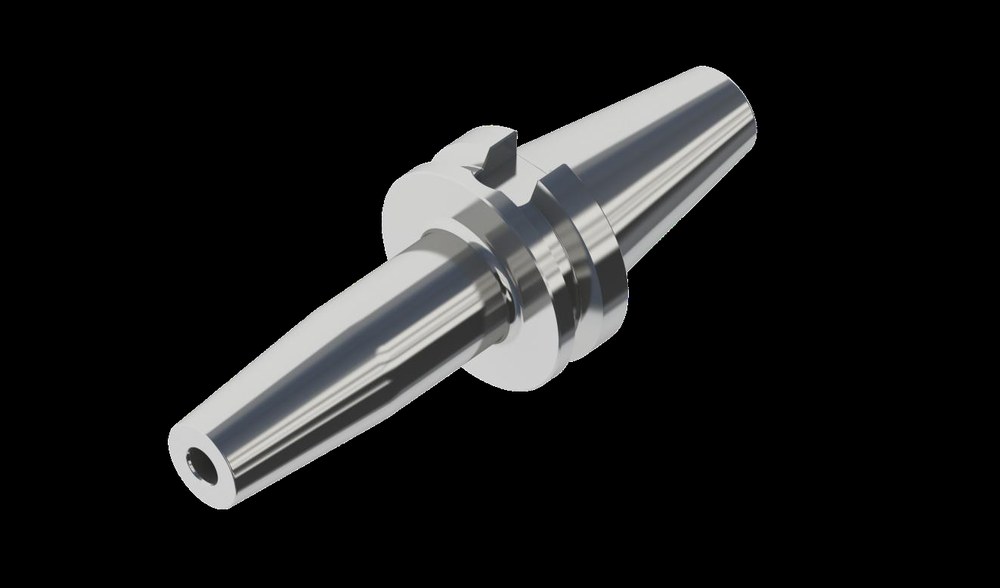
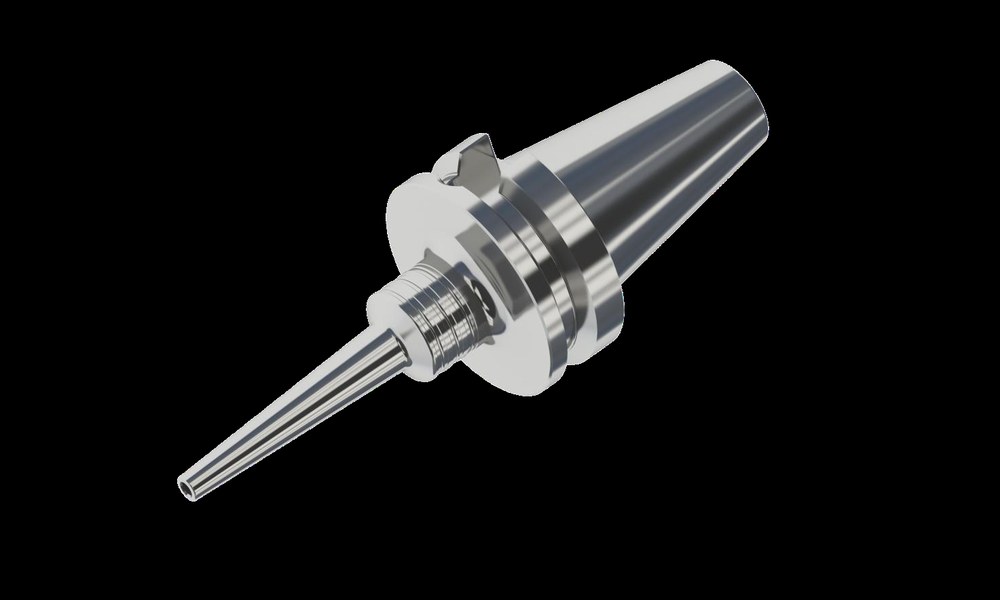
Two material families covering every scenario: robust alloy steel for heavy cutting, and special stainless steel for the slimmest, longest-life holders on the market.
Alloy steel holders are produced by major European and American tooling brands. Stainless steel holders use a special martensitic stainless steel — originally developed by MST of Japan — and our dimensions follow the MST standard.

| Material | Special alloy steel |
| Hardness | HRC 52–54 |
| Heating temperature | 450–600 °C |
| Corrosion resistance | Moderate (maintain regularly) |
| Heating method | Induction |
| Profile | Robust — ideal for heavy cutting; heavy-duty type on request |
| Price | Economical |

| Material | Taper: martensitic SS 4Cr13 · Grip: special stainless |
| Hardness | Taper HRC 52–54 · Grip HRC 40–45 |
| Heating temperature | 250–400 °C (safer, no overheat damage) |
| Service life | ≈ 5,000 tool changes |
| Heating method | Induction or hot-air (universal) |
| Profile | Slim & CV-curve types, wall from 1.5 mm — deep cavity / 5-axis |
| Price | Premium (special material) |
Holder length ≤ 100 mm: 0.003 mm · 120 mm: 0.004 mm · 150 mm: 0.005 mm.
Higher balancing grades available on request.
Standard versions offer extended gripping depth; slim stainless types start at 3 mm single wall (alloy) / 1.5 mm (stainless).
Balancing adjustment holes and special dimensions available as made-to-order items.
Shrink fit works on the thermal expansion difference between holder and tool, so only carbide (tungsten steel) tools with tight shank tolerances can be used. HSS tools expand together with the holder and cannot be removed. Tools must be inserted to the minimum gripping depth or deeper, and must not touch the holder bottom.
| Shank Ø (mm) | Tolerance zone | Tolerance (mm) |
|---|---|---|
| 4 | h4 | 0 / −0.004 |
| 5 | h5 | 0 / −0.005 |
| 6 | h6 | 0 / −0.008 |
| 8 | h6 | 0 / −0.009 |
| 10 | h6 | 0 / −0.009 |
| 12 | h6 | 0 / −0.011 |
| 16 | h6 | 0 / −0.011 |
| 20 | h6 | 0 / −0.013 |
| 25 | h6 | 0 / −0.013 |
⚠ Taps often have wider shank tolerance ranges — verify shank tolerance before shrink fitting.
Take off rubber-sealed inner-coolant tubes before heating to protect the seals. For BT holders, always use through-hole retention knobs so air can escape.
Chip residue burns onto the bore at high temperature and corrodes it. Clean with the dedicated bore brush — keep the bore free of chips and oil before every tool change.
Blow the holder dry with air, especially the bore, after water-cooled machining. For storage, remove the tool and apply rust-preventive oil — even stainless types rust without care.
BT30 / BT40 / BT50, HSK63A and more — tell us your taper and tool diameters for a same-week quotation.