★ Bookmark this site — the link never changes
Factory-direct precision tooling · Guangzhou, China WeChat only: 138 2401 0643 · cjjcjj536453360@163.com

Precision Shrink Fit Tool Holders for High-Speed Machining

Simple structure, superior balance, and unbeatable rigidity. Alloy steel and stainless steel shrink fit holders — plus matching induction heating machines — machined and balanced in-house.

≤0.003 mmTool runout (L ≤ 100)
G2.5 @ 25krpm balancing grade
100 N·mClamping force @ Ø10
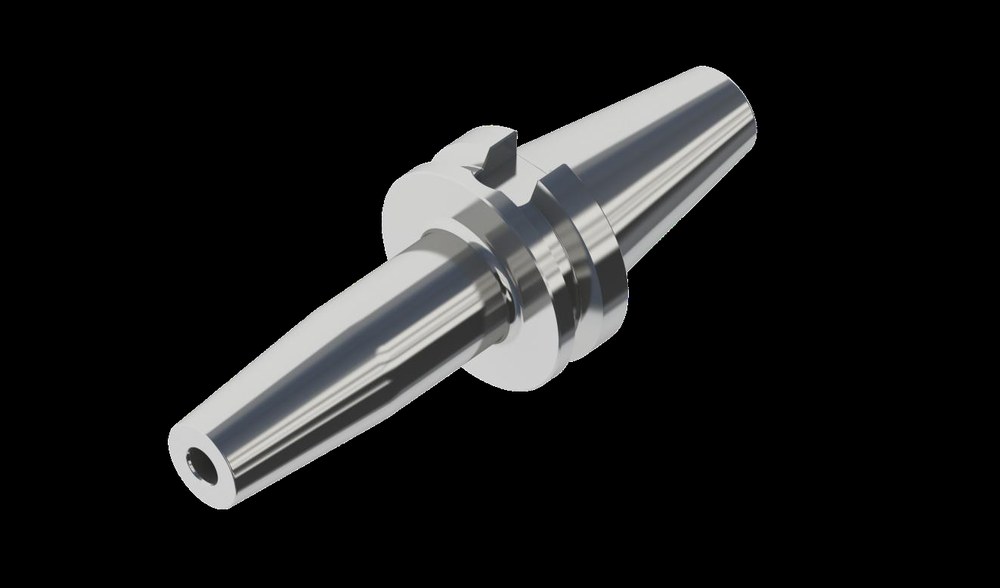
Shrink fit tool holders BT30 / BT40
0.003mm max runout — the accuracy of a solid piece of steel
2.6×higher rigidity vs. ER collet chucks
5000+tool changes (stainless steel type)
1.5 mmminimum wall — the slimmest holder available
Why Shrink Fit

No nuts. No collets. No compromise.

A shrink fit holder grips the tool by thermal contraction — the bore is expanded by heating, the carbide tool is inserted, and cooling locks it with uniform radial pressure. With no extra clamping parts, it outperforms conventional collet chucks in every dimension that matters.

◎

Higher Accuracy

Runout of ≤0.003–0.005 mm depending on holder length. No nut or collet errors — ideal for fine finishing.

≡

Better Balance

Smooth, slot-free profile with factory-set balancing G2.5 @ 25,000 rpm that never changes. Built for high-speed spindles.

⟂

Slimmest Profile

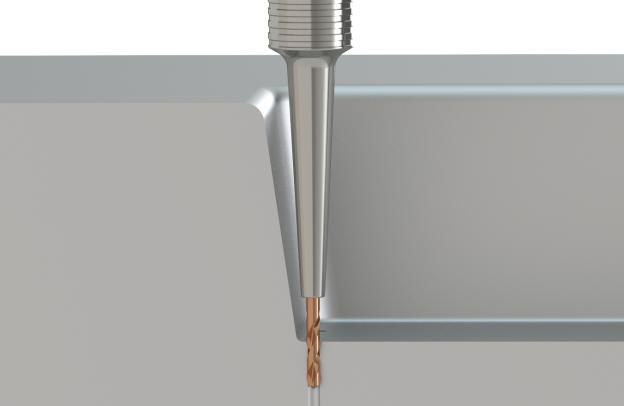
Wall thickness down to 1.5 mm. The most compact holder type on the market — perfect for deep-cavity and 5-axis work.

⇅

Stronger Grip

Up to 100 N·m clamping force at Ø10 — more than double a typical ER collet chuck (~45 N·m). Shorter tool overhang adds rigidity.

◔

Lower Air Resistance

The perfectly round exterior reduces windage at extreme spindle speeds — another reason it excels in HSC machining.

✓

Simple & Durable

One holder, one tool diameter, nothing to wear out or re-adjust. Stainless steel type delivers 5,000+ heating cycles.

How It Works

Thermal expansion, locked by physics

The holder bore and the carbide tool have very different thermal expansion coefficients. Heating the holder expands the bore; as it cools, it clamps the tool with immense, perfectly centered force.

1 · Heat the holder

The induction heater expands the holder bore in seconds — 450–600 °C for alloy steel, 250–400 °C for stainless steel.

2 · Insert the tool

Drop the carbide tool (h4–h6 shank tolerance) in to its minimum gripping depth while the bore is expanded.

3 · Cool & clamp

As the holder cools, the bore contracts uniformly around the tool shank — a rigid, high-accuracy, vibration-free connection.

Note: only carbide (tungsten steel) tools can be used. HSS tools expand with the holder when reheated and cannot be removed.

Product Lines

Two holder families. One matching machine for each.

Choose alloy steel (German-style) for heavy cutting and value, or special stainless steel (Japanese-style) for slim profiles, lower heating temperature and long service life.

Alloy steel shrink fit holder

Alloy Steel Shrink Fit Holders

Robust profile with excellent rigidity for heavy cutting. HRC 52–54, heating 450–600 °C, G2.5 @ 25,000 rpm. Standard & heavy-duty types.

HRC 52–54Heavy cuttingCost-effective

Details →

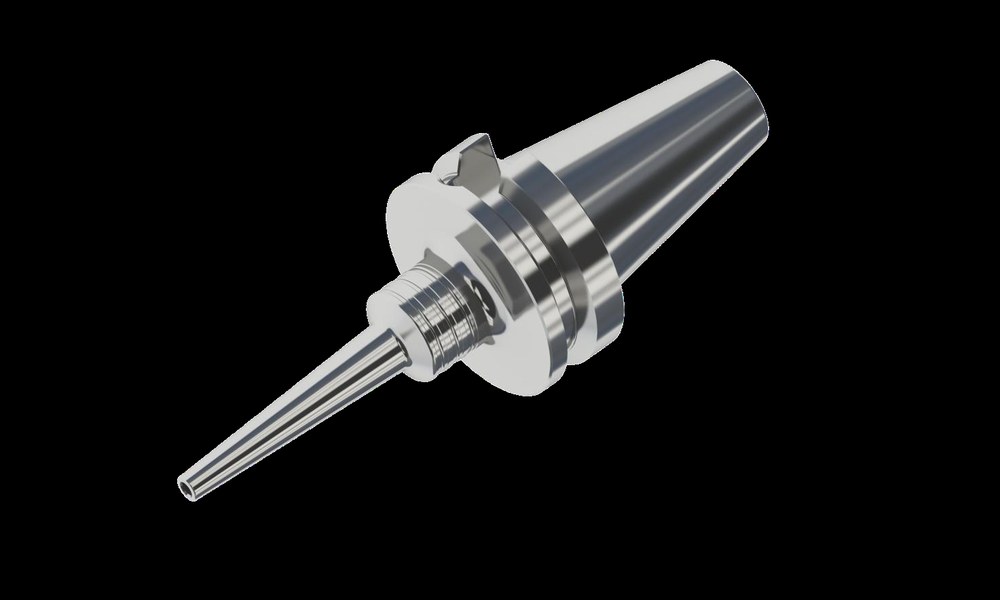
Stainless steel slim shrink fit holder

Stainless Steel Shrink Fit Holders

Slim & CV-curve types with walls down to 1.5 mm. Lower heating temperature (250–400 °C), ~5,000 tool changes, MST-compatible dimensions.

Wall ≥1.5 mm5000 cyclesDeep cavity

Details →

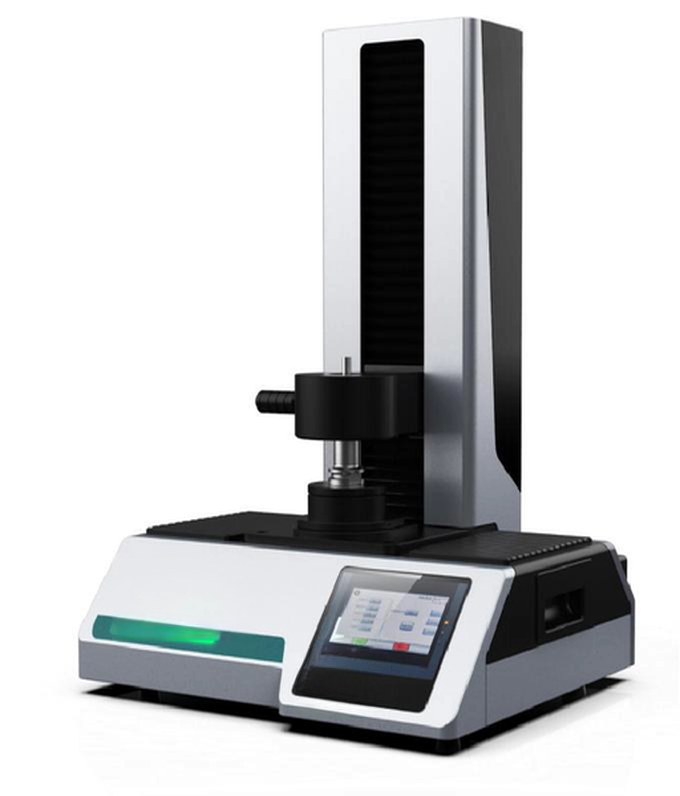
Shrink fit heating machine M-420

Shrink Fit Heating Machines

A-420 for alloy steel, S-420 for stainless, and M-420 for both materials. 7″ touchscreen, auto & manual modes, powerful air cooling.

A-420 / S-420 / M-420Dual-materialAuto mode

Details →

Applications

Where shrink fit wins

From 5-axis impeller finishing to deep mold cavities, shrink fit holders deliver the accuracy, reach and rigidity that collet chucks cannot.

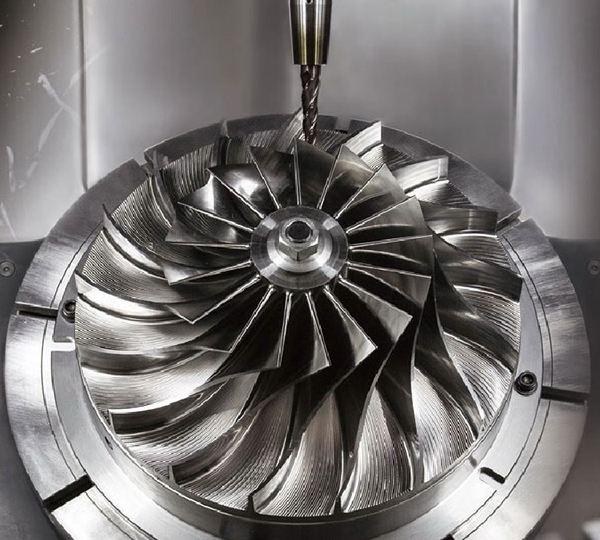
Impeller machining

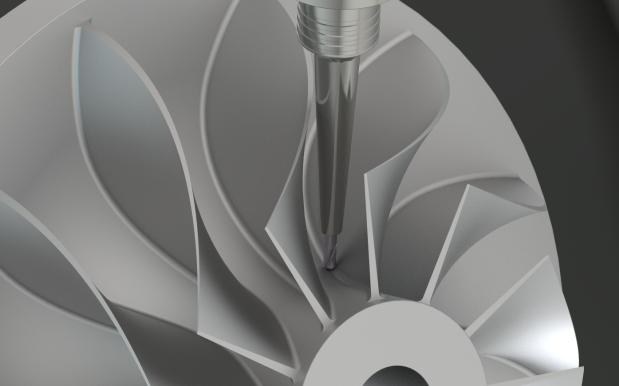
Impeller / Turbine

5-axis simultaneous machining of compressor wheels with slim holders.

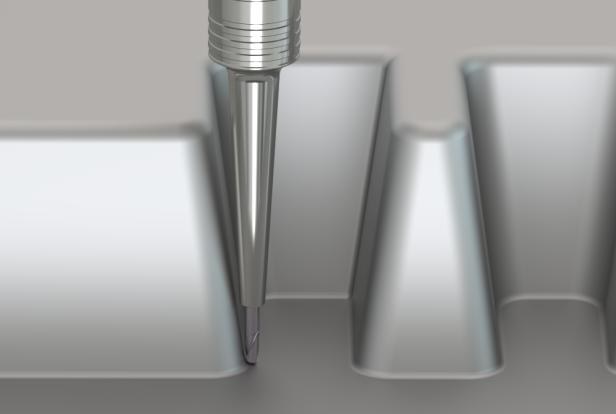
Mold cavity finishing

Mold & Die

Deep cavities and corners with minimal interference and fine finishes.

Narrow slot drilling

Deep-Cavity Finishing

Walls from 1.5 mm reach where no other holder fits.

5-axis precision machining

High-Speed Finishing

Perfect balance and low windage for high-RPM surface quality.

Explore all applications

Need a recommendation for your parts?

Send us your workpiece, spindle taper (BT / HSK / DIN) and tool diameters — our engineers will propose the right holder set within 24 hours.

Talk to an Engineer
WeChat only — no WhatsApp

Add us on WeChat by searching the phone number below, or email cjjcjj536453360@163.com. Every email is answered within 24 hours.

138 2401 0643
We do not use WhatsApp.